
More efficiency, less strain, no more turning
King optimizes large cladding panels with the RAS UpDownCenter 2
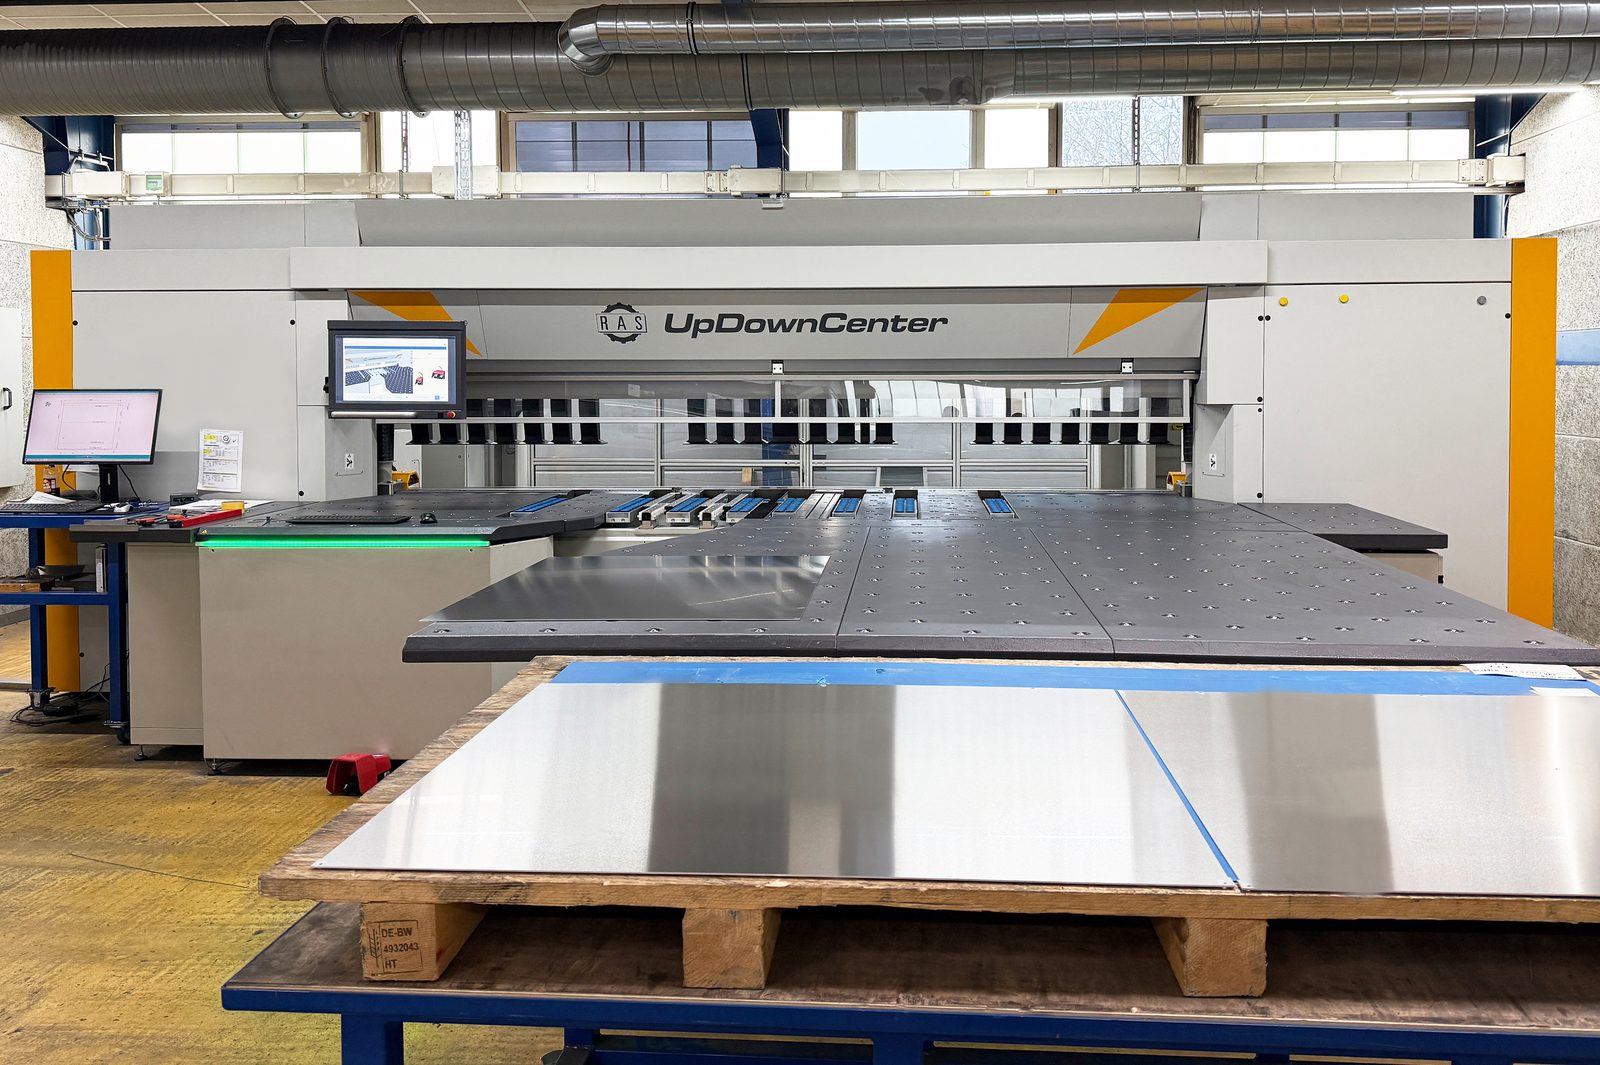
Less physical strain, much easier handling and noticeable time savings when forming Z-bends: King GmbH in Fluorn-Winzeln, Germany, now produces large-format cladding panels on the RAS UpDownCenter 2.
- up to 50%fewer operators for bending large parts
- zerosheet turning for Z-bends
- 4 mbending length up to 3 mm sheet
- a few daysof training instead of months
With the RAS UpDownCenter 2, King GmbH has taken the production of large-format cladding panels to a new level. Less physical strain, much easier handling and noticeable time savings when forming Z-bends show how much modern metal folding technology changes everyday work.
The results at a glance
- Z-bends without turning the sheet
- Up to 50% fewer operators for bending large parts
- Training in a few days instead of months
- Radii and step bends broaden the parts range
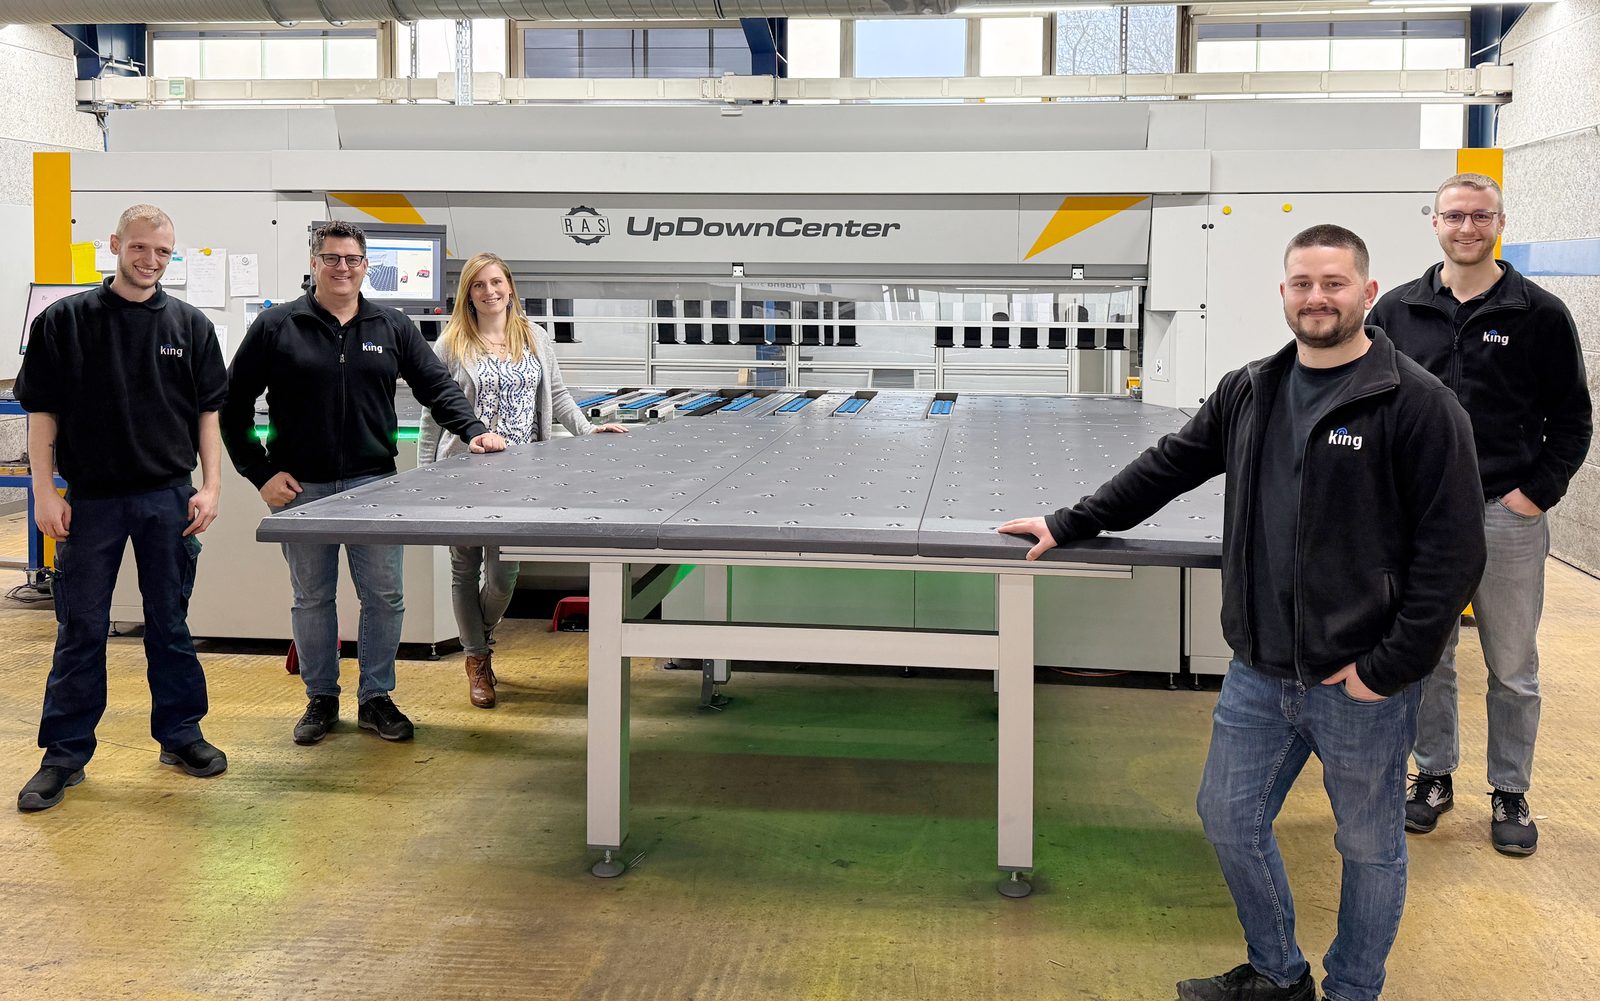
King GmbH, based in Fluorn-Winzeln, works in mechanical engineering and general sheet metal fabrication. The company produces machine enclosures, inner cabins, cladding panels, functional assemblies and individual parts. At two sites it develops customer-specific solutions, often involving large components such as machine tool enclosures and machine doors.
The challenge of press braking large parts
Most of these parts contain Z-bends that serve both as stiffeners and as functional elements. Until now they were produced on press brakes, which took considerable effort, especially with large sheets.
“With large sheets in particular, it takes an enormous amount of strength and carries a corresponding risk of injury,” says Marc Schrickel, Managing Director at King. For every Z-bend, the sheet had to be turned 180 degrees. With large formats, this often required a second person, meaning extra labor, heavy physical strain and growing fatigue in day-to-day work.
Clear requirements and a structured decision
King knew early on which direction the solution had to take. “It was always a given that we needed a 4-meter folding machine. Many suppliers simply couldn’t deliver that with our requirements.”
At Blechexpo 2021, the company gained an overview of the market and compared several suppliers. In-depth talks followed, including at RAS Reinhardt Maschinenbau in Sindelfingen, along with a look at production in Wildberg-Effringen. “We were pleasantly surprised by the high level of in-house manufacturing. RAS makes the key components itself.”
Being able to test sample parts on site was another important point. Alongside the 4-meter bending length and material thicknesses up to 3 mm, it was the overall package of machine, software and personal support that won King over. “The collaboration was simply a good fit, too. RAS was clearly ahead in the comparison.”
The UpDownCenter 2 as a powerful bending center
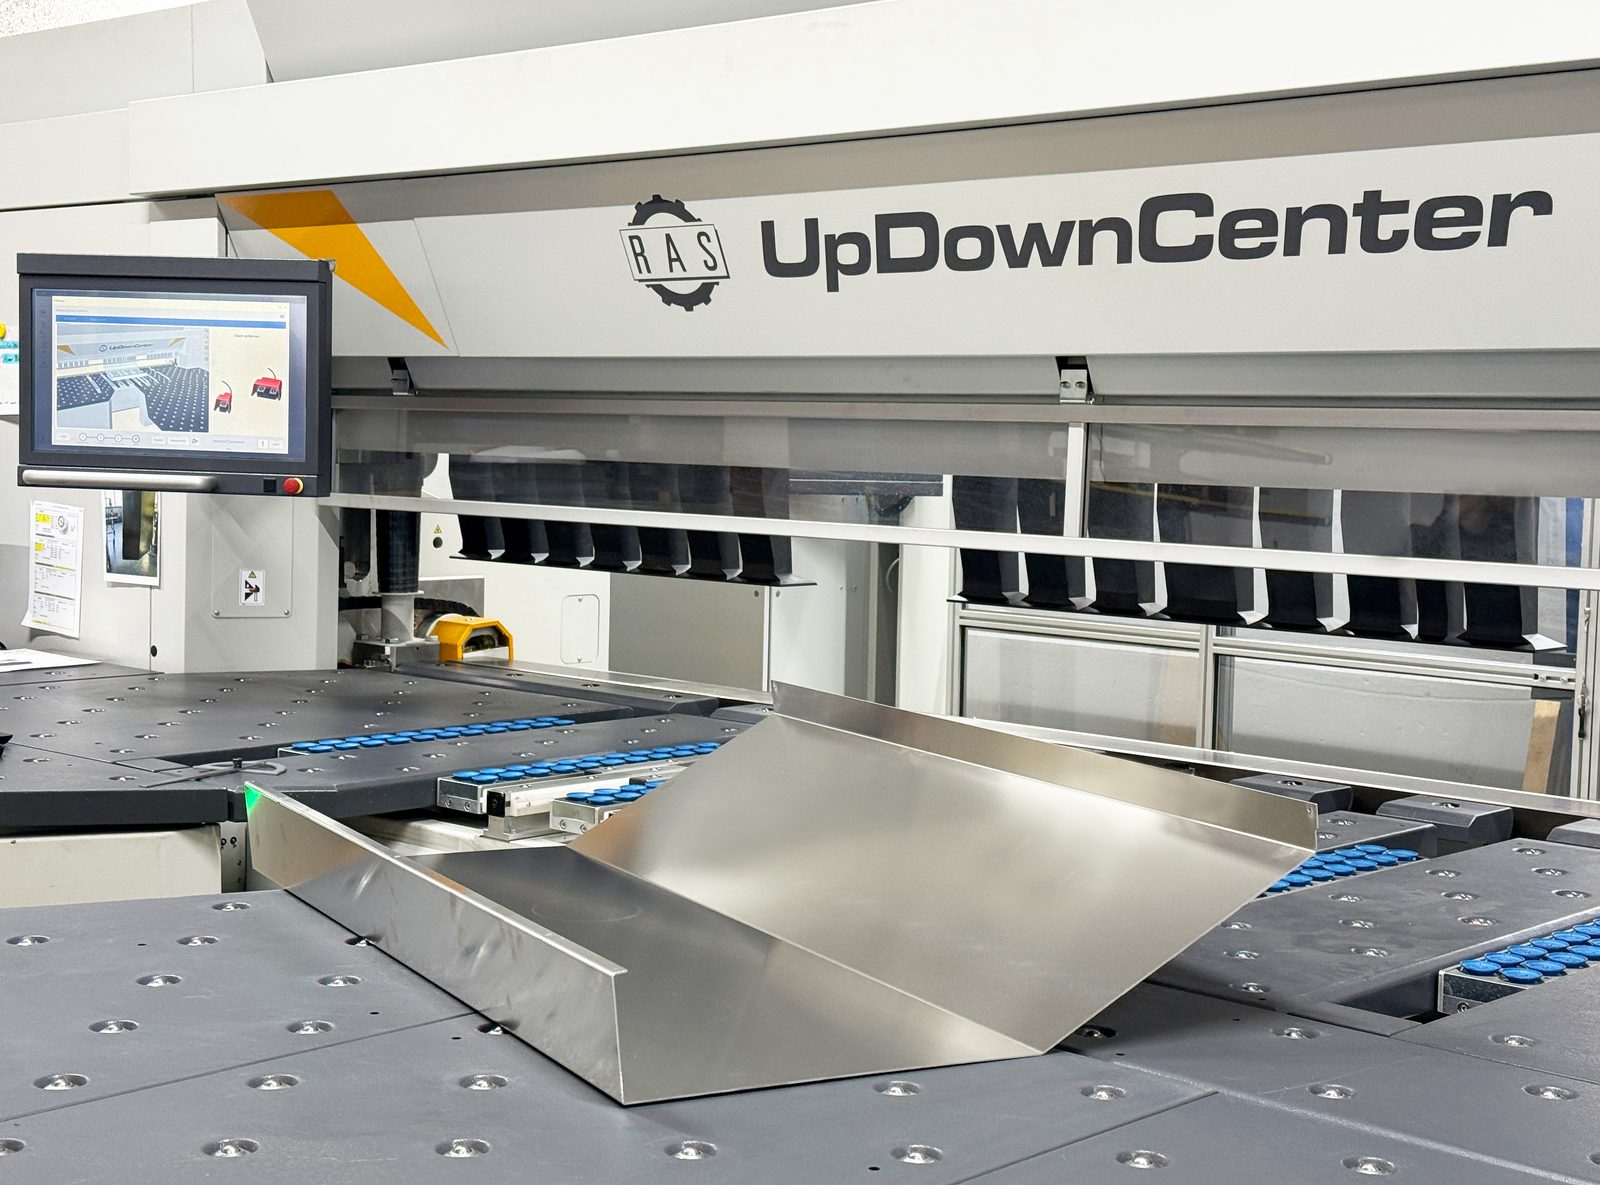
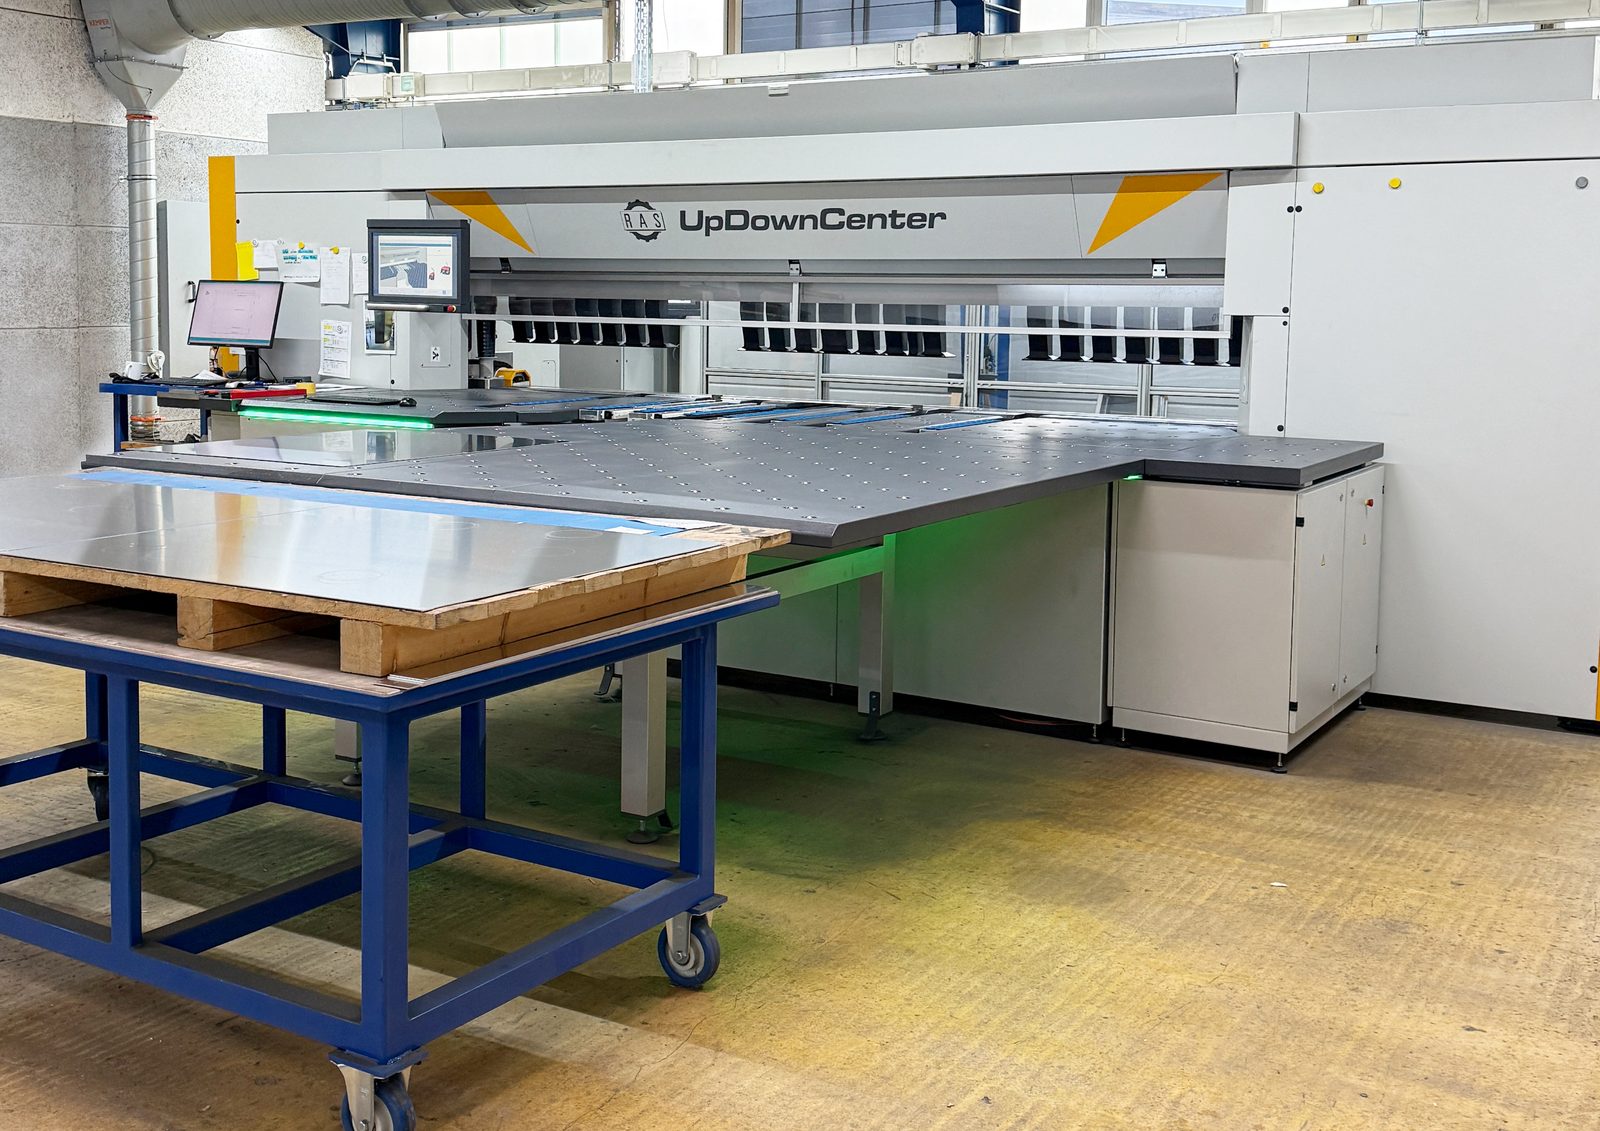
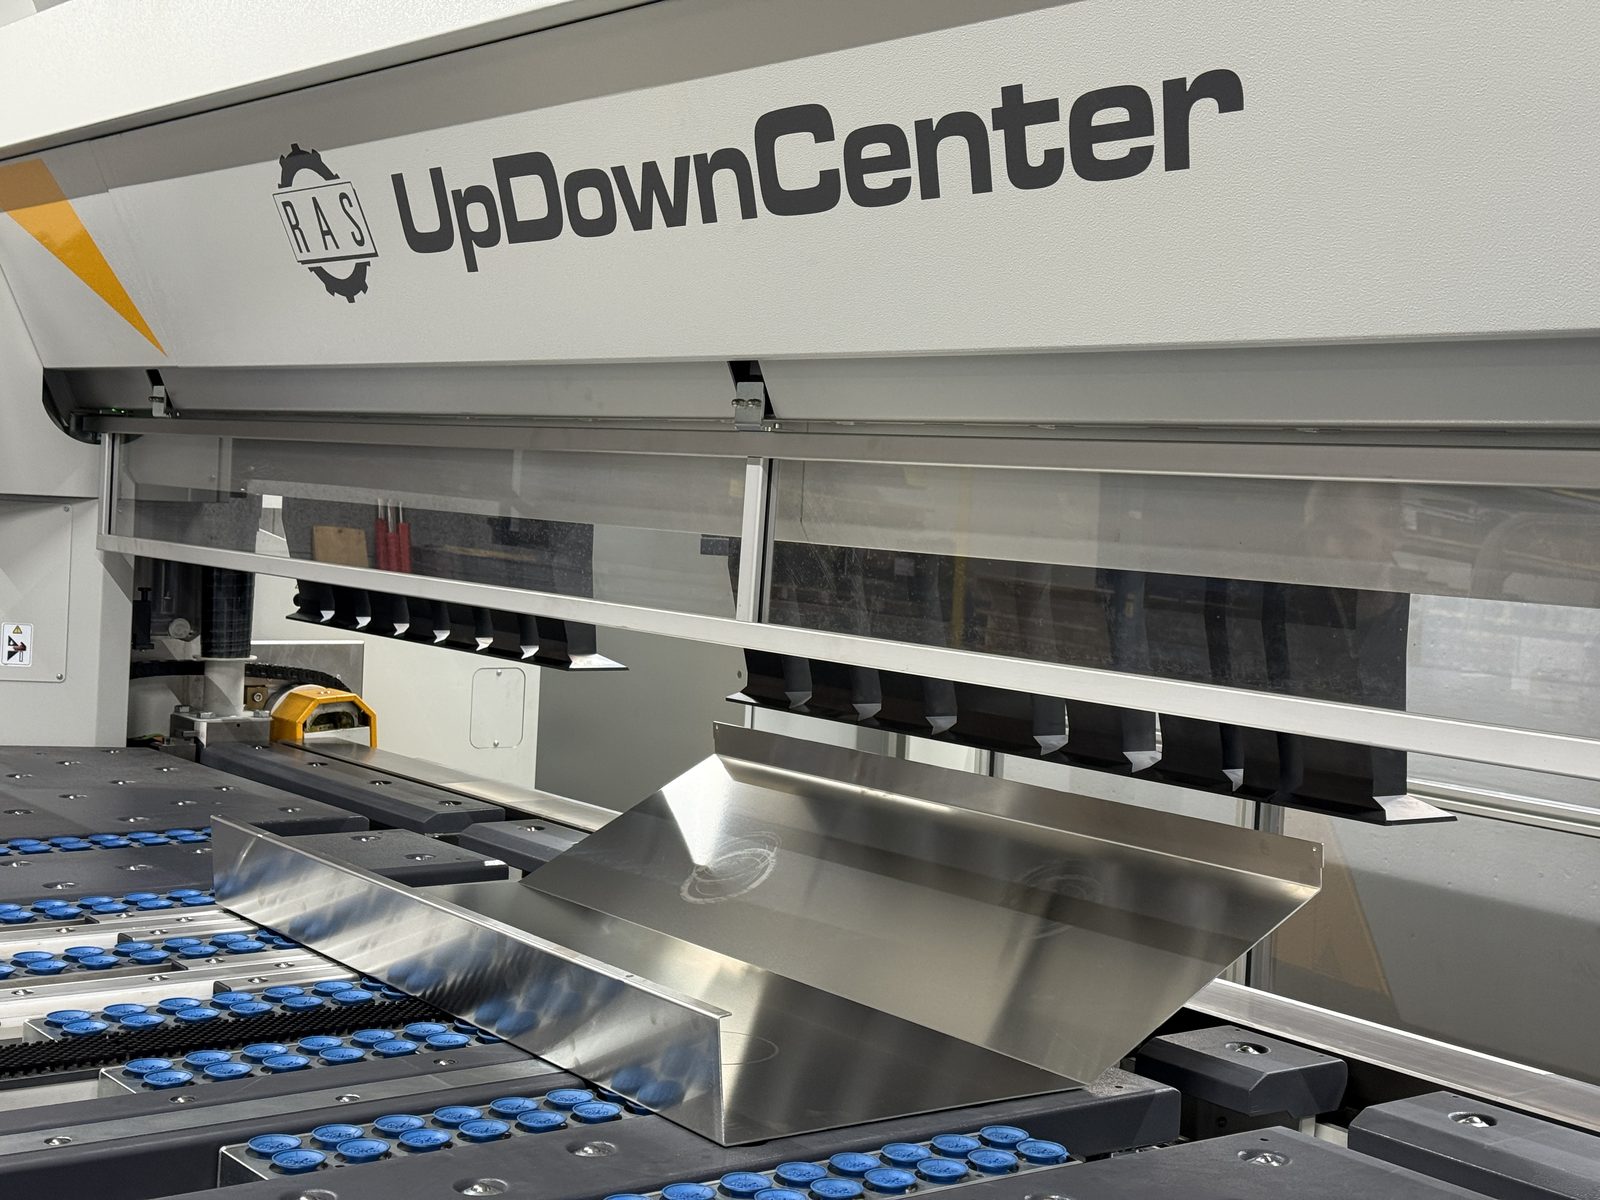
With the UpDownCenter 2, King relies on a semi-automatic bending center for large and demanding sheet metal parts. With bending lengths up to 4 meters and material thicknesses up to 3 mm, the machine is designed for the panels and boxes needed for cladding and machine enclosures.
The extra-large support table with integrated ball rollers ensures safe, ergonomic handling even of large blanks. The table surface of around 5 x 4 meters carries the full weight and noticeably relieves the operator. Combined with consistently high bending force across the entire working length, the result is a stable process for large-format parts.
Efficient bending without turning
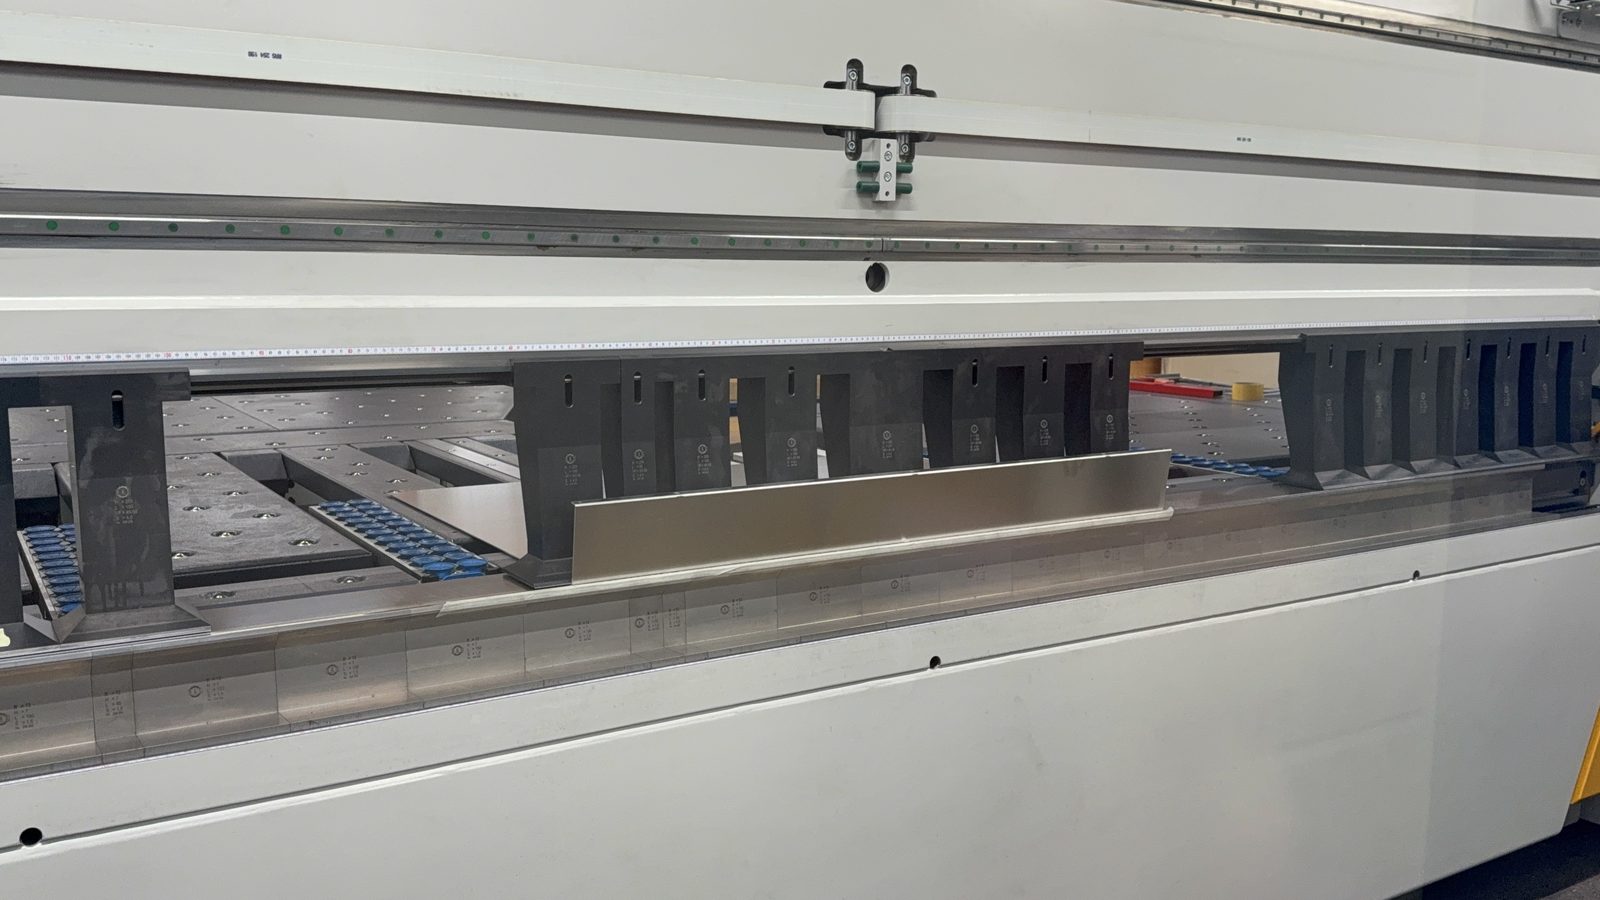
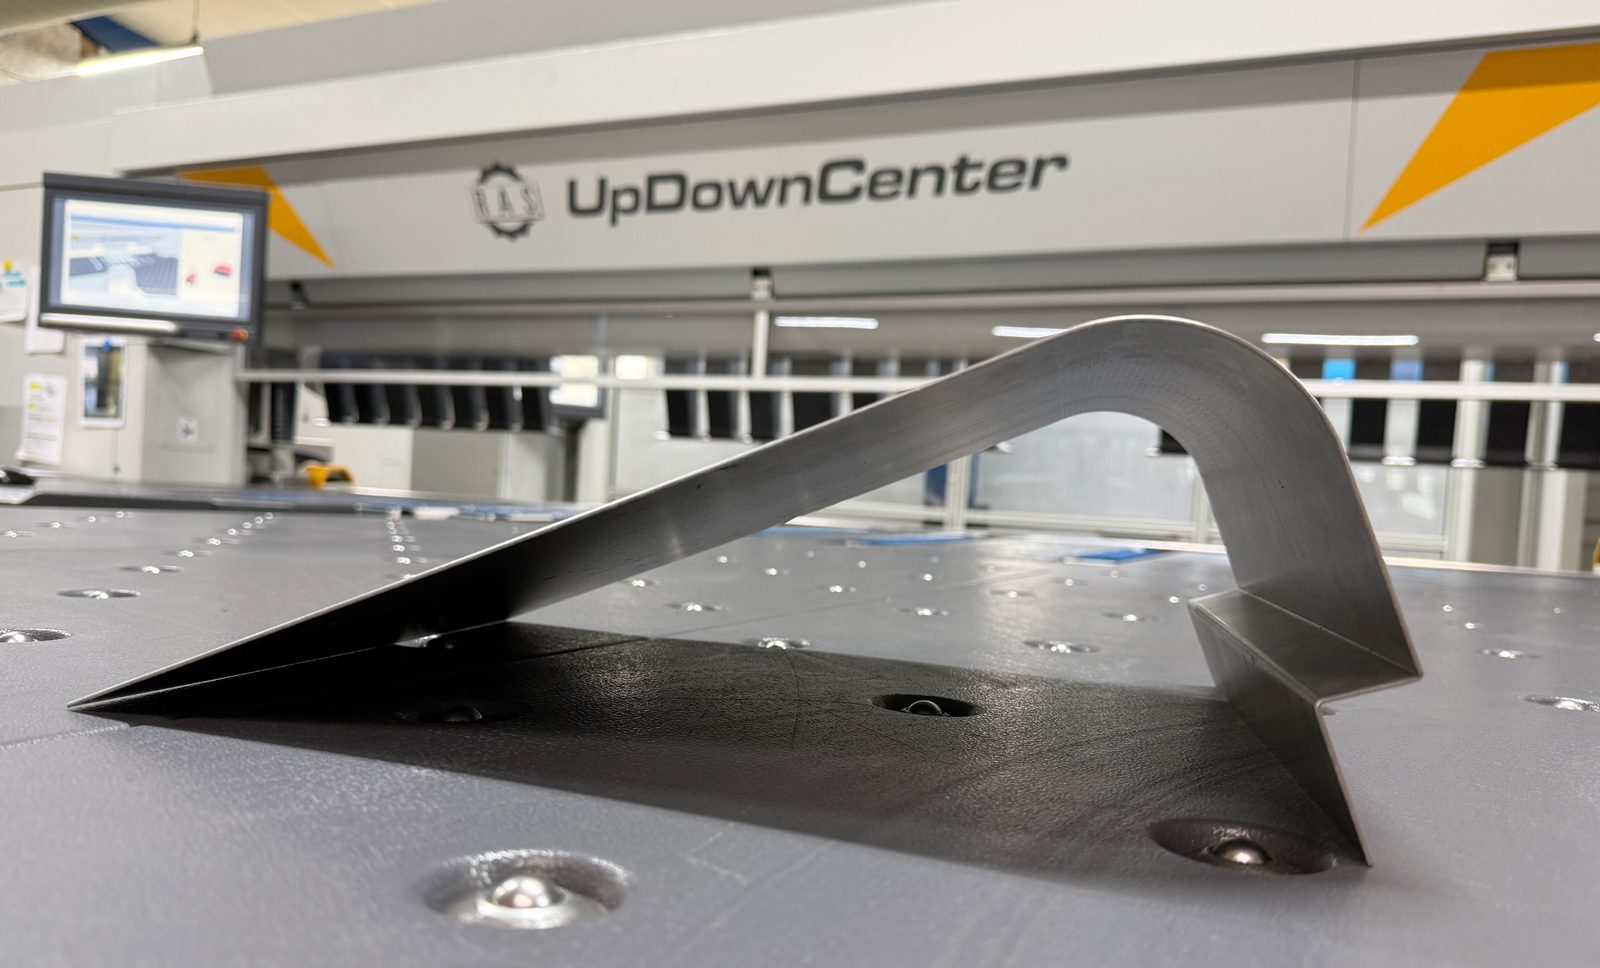
With the UpDownCenter 2, King has removed its biggest bottleneck: there is no more turning of sheets. Thanks to UpDown bending technology, the part stays in one position throughout the process.
At the same time, staffing requirements have dropped considerably. Whereas large parts often had to be handled by two people on the press brake, one person can now do the job in many cases. That is a saving of up to 50 percent in labor for this process step. Workflows are more efficient, safer and much calmer in daily operation.
“With large sheets in particular, it takes an enormous amount of strength and carries a corresponding risk of injury.”Marc Schrickel, Managing Director, King GmbH, on press braking
Fewer errors and faster training
Metal folding also has clear advantages in operation. New employees can run the machine within a few days. “On a press brake it takes much longer. You’re talking more like months,” says Marc Schrickel.
The potential for errors has also fallen noticeably. Whereas press braking involves many influencing factors, metal folding is far more stable and reproducible, which has a direct impact on quality and process reliability.
More flexibility in production
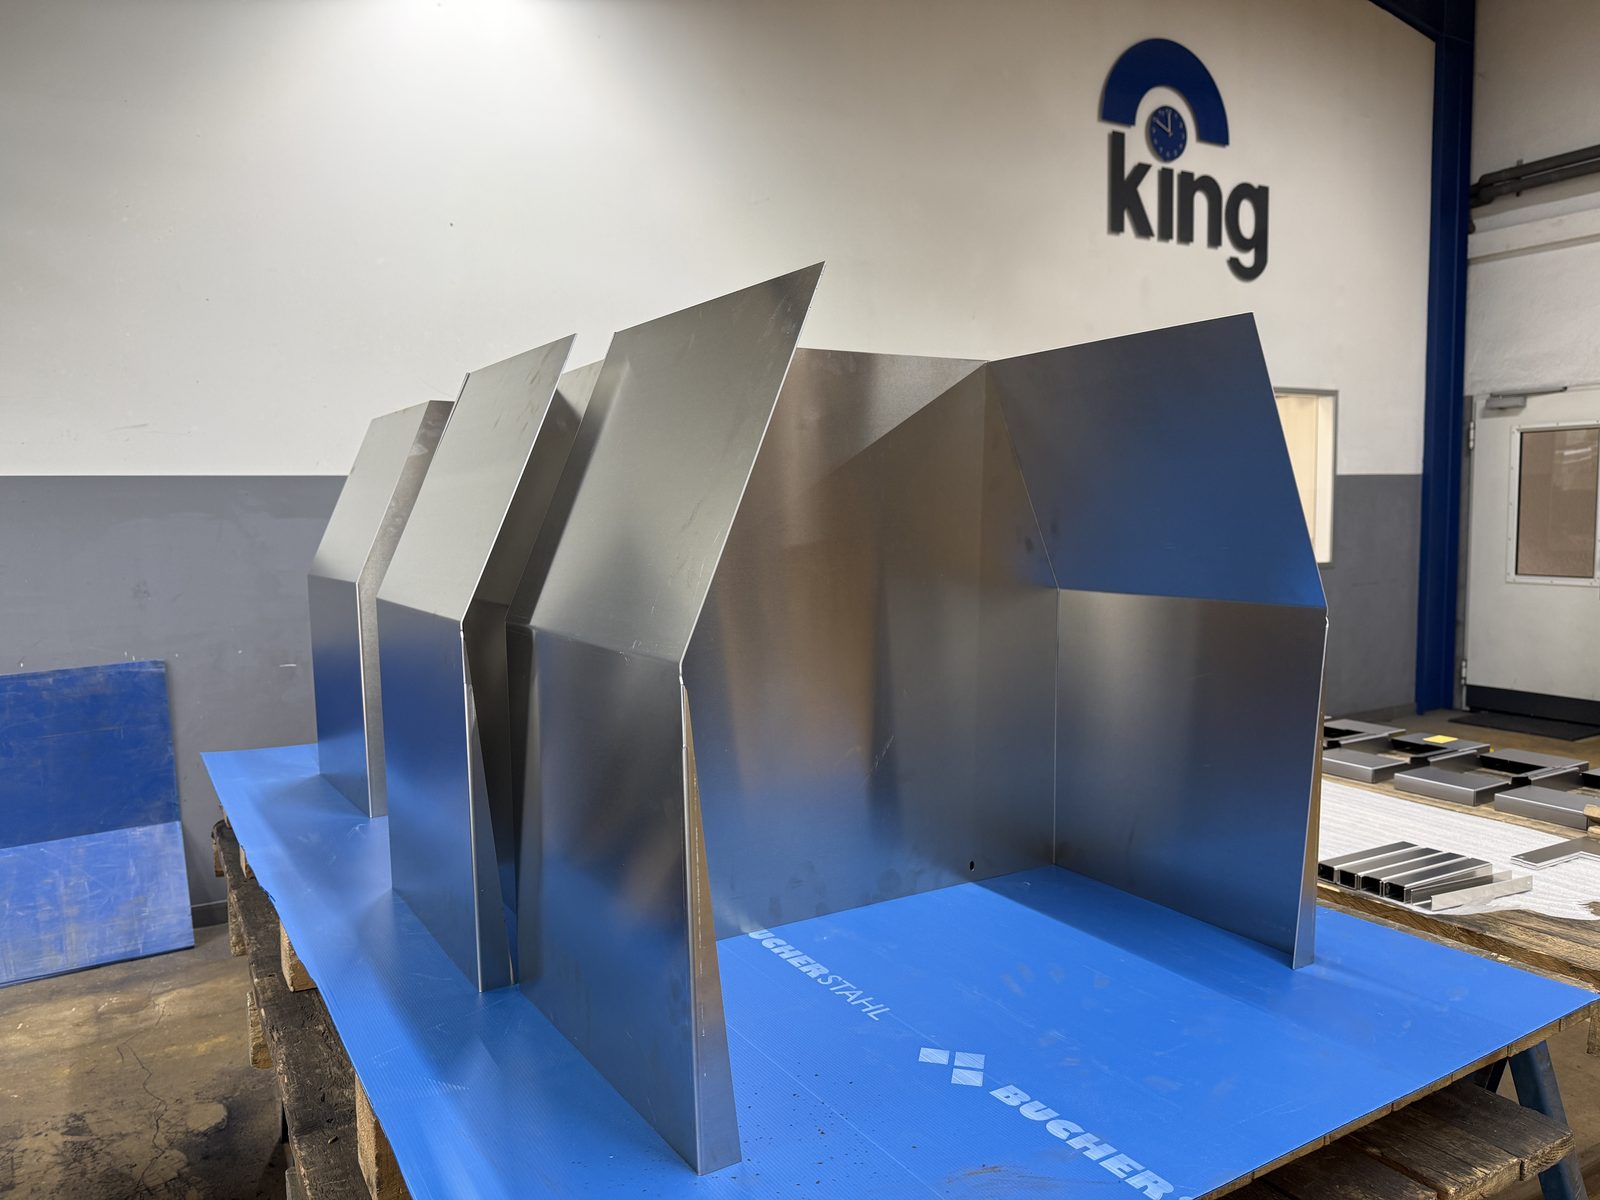
Besides efficiency, King has gained flexibility. Radii and step bends are easy to produce and significantly broaden the parts range, opening up new design options for complex cladding parts in particular.
This is supported by an integrated software solution from the office to the machine. Programs are created efficiently at the desk and sent straight to production. “The interplay between software and machine simply works.”
A clear decision for greater efficiency
With the RAS UpDownCenter 2, King has taken its production a decisive step forward. Processes now run more efficiently and stably and are much easier to handle, especially for large-format parts.
“For us, it was the right decision. In a direct comparison with the market, RAS clearly convinced us.”Marc Schrickel, Managing Director, King GmbH
King has a clear recommendation for anyone who wants to see for themselves: “A visit to RAS Reinhardt Maschinenbau in Sindelfingen and a look at production in Wildberg is definitely worth it.”
Inside production at King
Do you bend large cladding panels?
Test your parts with us. We will show you in Sindelfingen how the UpDownCenter 2 produces them without turning.